Precision-Engineered Machinery for Automotive Maintenance, Heavy Deep Drawing, and Automated Assembly
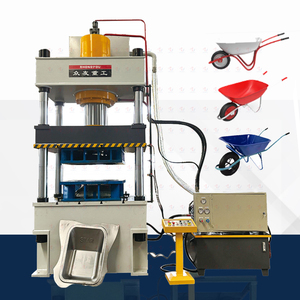
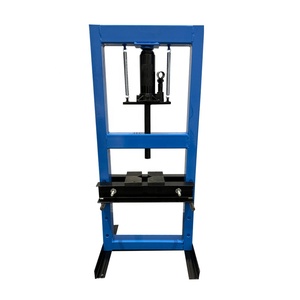
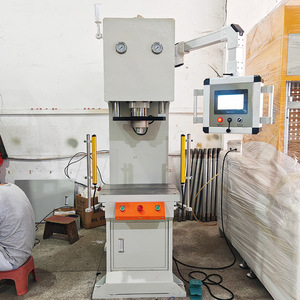
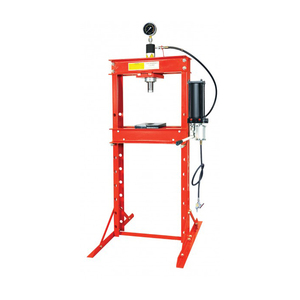
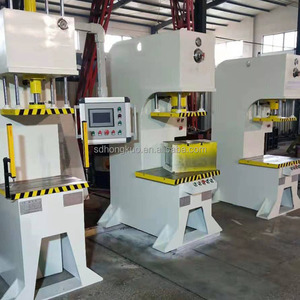
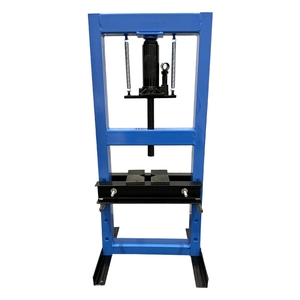
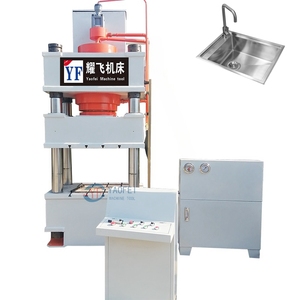
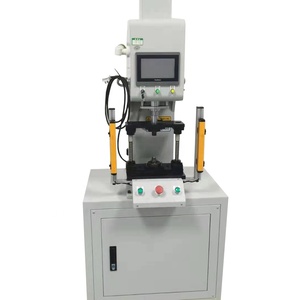
In modern industrial manufacturing, selecting a qualified CE certified bearing press manufacturer requires an in-depth audit of structural design parameters, European Union safety directive compliance, and precision force-displacement monitoring capabilities. A bearing press is not merely a force-generating cylinder; it is an integrated mechanical system engineered to seat rotational rolling elements into precise housing bores without inducing microscopic race damage, brinelling, or shaft deformation.
Full compliance with the European Machinery Directive 2006/42/EC mandates rigorous risk assessment methodologies, strict adherence to EN ISO 16092-3 (Safety of Machine Tools — Presses — Part 3: Hydraulic Presses), and compliance with the Low Voltage Directive (LVD) 2014/35/EU and Electromagnetic Compatibility (EMC) Directive 2014/30/EU. Premium press original equipment manufacturers (OEMs) implement dual-channel safety light curtains, Category 4 / PL e safety relays, and redundant hydraulic anti-drop block valves to guarantee operational safety across multi-shift production environments.
Technical Insight: Information Gain on Bearing Failure Mechanisms
Improper installation force accounts for over 16% of premature bearing failures according to ISO 15242 standards. CE certified press machinery utilizing real-time load-cell displacement monitoring prevents over-travel and eccentric seating, effectively mitigating subsurface fatigue and micro-welding in high-speed automotive and aerospace assemblies.
Heavy-gauge Q355B welded steel H-frames and single-column frames are subjected to stress-strain FEA simulations to guarantee structural deflection remains below 0.05mm/m under peak 400T loads.
Electro-servo actuators integrate AC synchronous motors coupled with high-precision planetary ball screws, delivering micro-meter position control (±0.01mm) and real-time press-fit curve output.
Equipped with Rexroth or Parker proportional hydraulic valves, hard-chromed ram shafts, and multi-stage polyurethane seals to eliminate fluid weeping and pressure drop during long dwell cycles.
Industrial procurement teams must evaluate press drive architectures based on target application requirements, production volume, cycle time, and energy efficiency. Below is an engineering comparison matrix designed to assist factory managers and system integrators in specifying the optimal press configuration:
| Performance Parameter | Hydraulic Shop & Floor Press (6T – 20T) | Industrial Hydraulic Press (315T – 400T) | Electric Servo Bearing Press (2T – 30T) |
|---|---|---|---|
| Target Application | Automotive workshop maintenance, bearing removal, general shop fitting | Deep drawing wheelbarrow trays, heavy cooker assembly, sheet metal forming | Automotive transmission assembly, electric motor bearings, electronic riveting |
| Positional Repeatability | ±0.50 mm (Manual / Air-hydraulic gauge control) | ±0.10 mm (Proportional valve PLC control) | ±0.005 mm (Closed-loop encoder system) |
| Force Monitoring Capability | Analog pressure gauge reading | Digital transducer display with limit switches | Real-time 100Hz Force vs. Stroke curve analysis (OK/NOK judgment) |
| Energy Efficiency Ratio | Standard intermittent motor power | Continuous motor idle; hydraulic oil heat loss | Power drawn only during ram stroke (>40% energy savings) |
| Noise Level & Maintenance | 68 - 75 dB / Oil replacement every 2,000 hrs | 72 - 82 dB / Hydraulic filter & seal servicing | < 62 dB / Clean-room friendly, minimal grease lubrication |
| CE Safety Certification | EN ISO 16092-3; Manual overload relief | EN ISO 16092-3; Dual optical guards & interlocking relays | EN ISO 16092-2/3; Integrated torque-limiter & emergency stops |
The global industrial press market is undergoing a structural transition driven by Industry 4.0 digitisation, decarbonisation mandates, and automated quality control integration. Procurement directors evaluating CE certified bearing press manufacturers should align their technical specifications with the following dominant industry trends:
Modern bearing press installations no longer operate as isolated islands of automation. Leading machinery manufacturers equip single-column, H-frame, and servo press systems with programmable logic controllers (Siemens S7-1500 or Mitsubishi FX5U) supporting fieldbus protocols such as PROFINET, EtherCAT, and OPC UA. This connectivity enables real-time telemetry streaming of peak force, insertion depth, dwell time, and cycle counts to centralized MES (Manufacturing Execution Systems), establishing digital traceability for critical components in electric vehicle (EV) drivelines and industrial gearboxes.
While traditional hydraulic presses remain indispensable for heavy-tonnage deep drawing operations (such as 315T to 400T wheelbarrow pan stamping or appliance housing forming), high-precision assembly lines are rapidly adopting electro-servo presses. The elimination of hydraulic fluid eliminates thermal expansion variables, avoids environmental oil contamination risks, and reduces factory floor ambient noise levels significantly.
Advanced press fit verification employs dynamic force-stroke windowing. As the press tool drives the bearing inner ring onto a shaft or outer ring into a housing bore, the machine controller maps the force curve against an envelope zone. If the shaft diameter is oversized, the force breaches the upper boundary; if the bore is loose or missing, the force drops below the lower limit. The system instantly halts the stroke, triggers an alarm, and logs the defective part, preventing downstream line stoppage.
As an established high-precision industrial press manufacturer, our production ecosystem is structured around strict ISO 9001:2015 quality management procedures and European CE compliance frameworks. Every machine—from benchtop 6-ton automotive shop presses to automated 400-ton hydraulic deep drawing presses—undergoes exhaustive structural, hydraulic, and electrical validation prior to dispatch.
Frame uprights, beds, and guided slides are machined on large-scale 5-axis CNC gantry milling centers to ensure parallelism within ±0.02mm across the entire bed surface.
Hydraulic manifolds undergo 24-hour static pressure holding tests at 125% rated capacity to verify seal integrity, hose burst safety margins, and valve responsiveness.
Our in-house engineering team designs and manufactures bespoke press-fit anvils, quick-change die sets, automatic ejectors, and rotary indexing tables tailored to your part drawings.
Technical Answers to Essential Machinery Selection, Operating, and Compliance Inquiries